Overview
Femtosecond laser microcutting eliminates the heat-affected zone (HAZ) entirely through cold ablation. Material is sublimated before thermal diffusion can occur, resulting in pristine edges without microcracking, recast layers, or burrs. The technology excels at cutting complex patterns in multi-layer materials where mechanical tools fail.
Physical Principle
The ultrashort pulse duration (< 500 fs) deposits energy faster than electron-phonon coupling time (~ps), preventing thermal diffusion to surrounding material. Peak powers in the gigawatt range enable nonlinear absorption in any material, regardless of linear optical properties. This enables cutting of transparent materials and selective layer removal in composite substrates.
Recommended CP-Series Models for This Process
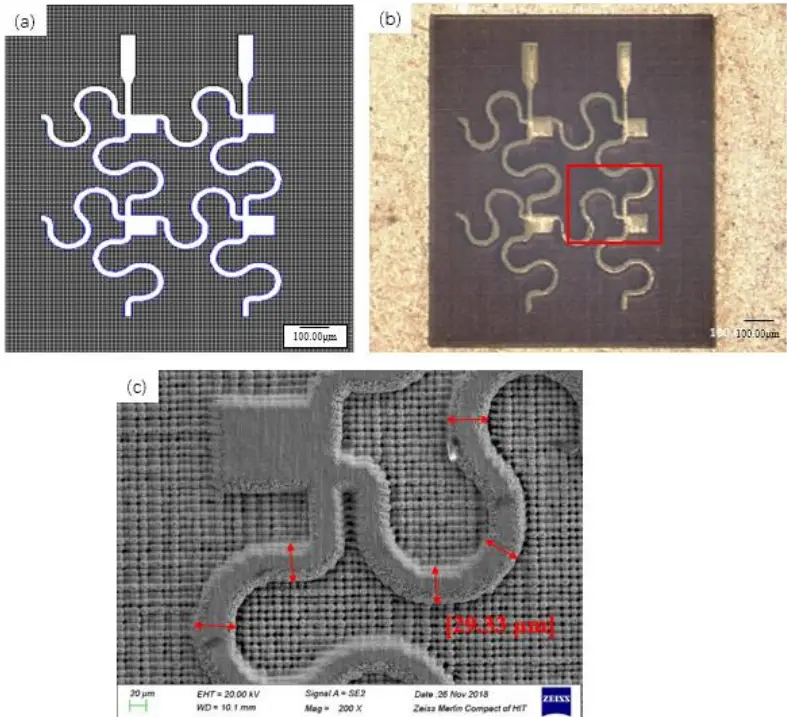
Femtosecond laser micromachining of flexible printed circuit boards (FPCBs). (a) CAD design pattern of display panel driving circuit, (b) optical microscopy of micromachined copper tracks on polyimide substrate showing clean ablation with no copper residues, (c) SEM image demonstrating high-fidelity curved features with 29.33 μm average track width and 0.67 μm machining accuracy. The complex patterns were achieved with 280 mW power and 39.5 kHz PRF, completely removing 35 μm copper layer without substrate damage. Reproduced from Lu et al., J. Phys.: Conf. Ser. 2185 012082 (2022). © 2022 The Authors. Licensed under CC BY 3.0.
Technical Capabilities
Compatible Materials
Glass (Borosilicate, Fused Silica)
No microcracking, clean edge breaks
Sapphire
HAZ-free cutting, maintains crystal integrity
Metals (Ti, Stainless Steel, Cu, Au)
No oxidation or burrs
Polymers (PMMA, PC, PEEK)
No charring or thermal deformation
Technical Ceramics (Al₂O₃, ZrO₂)
Minimal chipping vs. mechanical tools
Diamond and DLC coatings
Precise scribing without graphitization
Applications
Medical Device Manufacturing
- •Coronary stent cutting from nitinol tubes
- •Needle tip shaping
- •Microcannula drilling
Microfluidics
- •Through-glass vias (TGV)
- •Inlet/outlet port drilling
- •Channel interconnects
Watchmaking & Precision Mechanics
- •Gear tooth cutting
- •Ruby bearing drilling
- •Balance wheel modifications
Aerospace & Defense
- •Fuel injector nozzles
- •Sensor apertures
- •Cooling hole arrays
Technology Comparison
| Parameter | Femtosecond Laser | Nanosecond Laser | Mechanical Drilling |
|---|---|---|---|
| Heat-Affected Zone | < 1 μm | 50-400 μm | N/A (tool wear debris) |
| Edge Quality (Ra) | < 0.5 μm | 2-5 μm | 1-3 μm |
| Minimum Hole Diameter | 1 μm | 10 μm | 50 μm (tool limit) |
| Microcracking (brittle materials) | None | Common | Severe |
| Post-Processing Required | No | Yes (chemical/mechanical) | Yes (deburring) |
Related Application Spotlight
Application Spotlight: Burst-Mode Femtosecond Micromachining: Deeper, Straighter Holes in Glass
A Photoniques overview of MHz and GHz burst-mode ultrashort laser processing explains how pulse trains change ablation in metals and bandgap materials, enabling deeper cylindrical holes in glass and practical routes for milling, drilling, and cutting.
Read Application SpotlightApplication Spotlight: High-Quality CFRP Micro-Hole Drilling with Spatially Modulated Femtosecond Laser
A new SLM-based femtosecond drilling strategy for CFRP reduces taper to 0.716 degrees and achieves 2.9 micrometer roundness through response-surface optimization and copper-foil-assisted processing.
Read Application SpotlightFemtosecond Laser Drilling in Sapphire: Achieving High-Aspect-Ratio Microstructures
Recent advances in femtosecond laser ablation for sapphire enable crack-free drilling, high-aspect-ratio microstructures up to 80:1, and hybrid laser-chemical techniques for microfluidic and aerospace applications.
Read Application SpotlightReady to Implement This Process?
Contact us to discuss rental options (from €5000/month), outright purchase, or to connect with our partner network for job shop processing and process development services (paid).